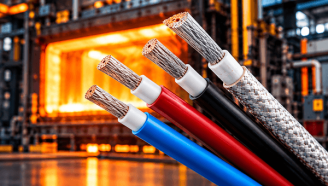
GN500 is an extreme high-temperature glass fiber cable with stranded pure nickel conductor. It features multi-layer fiberglass/mica tape insulation, glass fiber sheath, and optional silicone resin or sintered PTFE outer coating. Rated 300/500V, it can operate up to 500°C in dry conditions. Pure nickel conductor delivers outstanding oxidation resistance at ultra-high temperatures. This RoHS compliant inorganic cable is widely used for fire-resistant wiring in furnaces, steel mills, metallurgy, chemical plants and high-heat industrial equipment.
GN800 is an ultra-high-temperature fire-resistant cable built with stranded pure nickel conductor. It adopts multi-layer insulation of high-temperature fiber and mica tape, fiber sheath and sintered PTFE outer coating. Rated 300/500V, it can work stably up to 600°C in dry conditions. Pure nickel conductor delivers superior oxidation resistance under extreme heat. RoHS compliant, this cable is widely used for high-temperature wiring in furnaces, metallurgy, chemical, glass and ceramic industrial facilities.
GNFR500-02 is a high-temperature fire-resistant cable with stranded nickel-plated copper conductor. It adopts double-layer insulation tape, glass fiber sheath and sintered PTFE outer coating. Rated 300/500V, it can operate reliably up to 300°C. The inorganic glass fiber sheath is non-combustible, chemically resistant and mechanically robust. With good oxidation resistance and RoHS compliance, this cable is widely used for high-temperature wiring in ovens, metallurgy, chemical and thermal processing equipment.
GNJ500-03 is a high-temperature fire-resistant cable featuring stranded pure nickel conductor, insulation tape, glass fiber sheath and sintered PTFE outer coating. Rated at 300/500V, it works reliably from -65°C up to 300°C. The inorganic glass fiber sheath is non-combustible, chemically stable and mechanically strong. Its pure nickel conductor delivers outstanding oxidation resistance under high heat, and the cable is RoHS compliant for industrial high-temperature wiring in ovens, furnaces and metallurgical facilities.
JG silicone rubber insulated wire uses flexible bare copper or tinned copper stranded conductor. It can work stably within -60°C ~ 180°C, with rated voltage 500V or 1000V. This silicone wire features soft texture, good elasticity, aging resistance, waterproof and mildewproof performance. It supports halogen-free and flame retardant options and meets RoHS requirements. Widely used for steel, aviation, shipbuilding, power plants, lighting, electric heating equipment, motor leads and other high-temperature wiring scenarios.
JGG high voltage silicone rubber insulated wire uses flexible bare copper or tinned copper stranded conductor. It can work stably within -60°C ~ 180°C, with high rated voltage options of 3000V, 6000V and 10000V. This silicone wire is ultra-soft, elastic and flexible, featuring good aging resistance, waterproof and mildew-proof performance. It supports halogen-free and flame-retardant versions and meets RoHS requirements. It is widely used for steel, aviation, shipbuilding, power plants, industrial lighting, electric heating equipment and other high-voltage high-temperature wiring applications.
This medical equipment wire is specially engineered for medical devices, available in 2–9 cores with conductor sizes ranging from 36 AWG to 10 AWG. It adopts silver-plated copper or silver-plated alloy conductors, PTFE insulation and high-density silver-plated braided shielding. The outer jacket is made of German imported medical-grade silicone rubber, with optional TPE, TPV or TPU. It supports autoclave high-temperature sterilization, delivers stable performance from -60°C to 200°C, and features LSZH, low friction, dust resistance and outstanding biocompatibility. It meets FDA and RoHS requirements, widely used for therapeutic, monitoring, rehabilitation and diagnostic medical instruments.
This multi-core hybrid watertight cable integrates power and signal transmission in one single cable. It delivers reliable hybrid transmission of communication signals and power signals at the same time. With full-directional watertight sealing in axial and radial directions, it features excellent water corrosion resistance and stable performance for repeated underwater use. It is widely used for submarine and submersible underwater communication systems.
This multi-core shielded watertight cable adopts multi-core shielding design to effectively block external electromagnetic interference and guarantee stable signal transmission. It features outstanding waterproof, seawater corrosion resistance, oil resistance, UV resistance and chemical resistance. With high tensile strength and good bending & abrasion resistance, it can be equipped with custom tensile reinforcement. It is widely applied for power and signal connection of submersible robots, ocean monitoring sensors and underwater communication systems.
This photoelectric hybrid integrated tow cable combines optical fiber and power conductors in one integrated cable. It supports synchronous transmission of optical signals and electric power for long-distance underwater missions. Built with multi-layer heavy-duty structure, it features outstanding tensile strength and pressure-resistant sealing. Designed for long-length use over 1km, it can withstand repeated launch and recovery cycles in harsh marine underwater environments.
PIR-350 is a high-temperature polyimide wire with nickel or nickel-plated copper conductor, helically wrapped PTFE tape insulation and polyimide tape sheath. It works continuously at 300°C and tolerates transient temperature up to 350°C, rated for 600V. Featuring outstanding heat-oxygen aging resistance, radiation resistance, mechanical strength and electrical insulation, it is non-hygroscopic, self-extinguishing and RoHS compliant. Widely used in hot runner molds, instrumentation, metallurgy, petroleum and chemical special high-temperature environments.
This rubber watertight communication cable is built for harsh underwater and marine environments. It delivers high tensile strength, excellent bending, abrasion, oil, UV, weak acid and seawater corrosion resistance, with reliable watertight performance. Customizable metallic or non-metallic reinforcing structures are available upon request. Adopting premium rubber materials and mature production technology, this cable prevents core breakage and jacket cracking, offering a service life 3–4 times longer than standard cables. It is widely used for signal transmission and interconnection in submarine and submersible communication systems to maintain stable signal links between internal transmitters and outside antennas.